Spiral Conveyor for Compact Vertical Product Flow
A spiral conveyor moves cartons, cases, and totes between elevations in a compact continuous path. Southwest Solutions Group helps evaluate container details, transfer points, clearances, and conveyor interfaces so the spiral conveyor system fits your facility layout.
What Is a Spiral Conveyor?
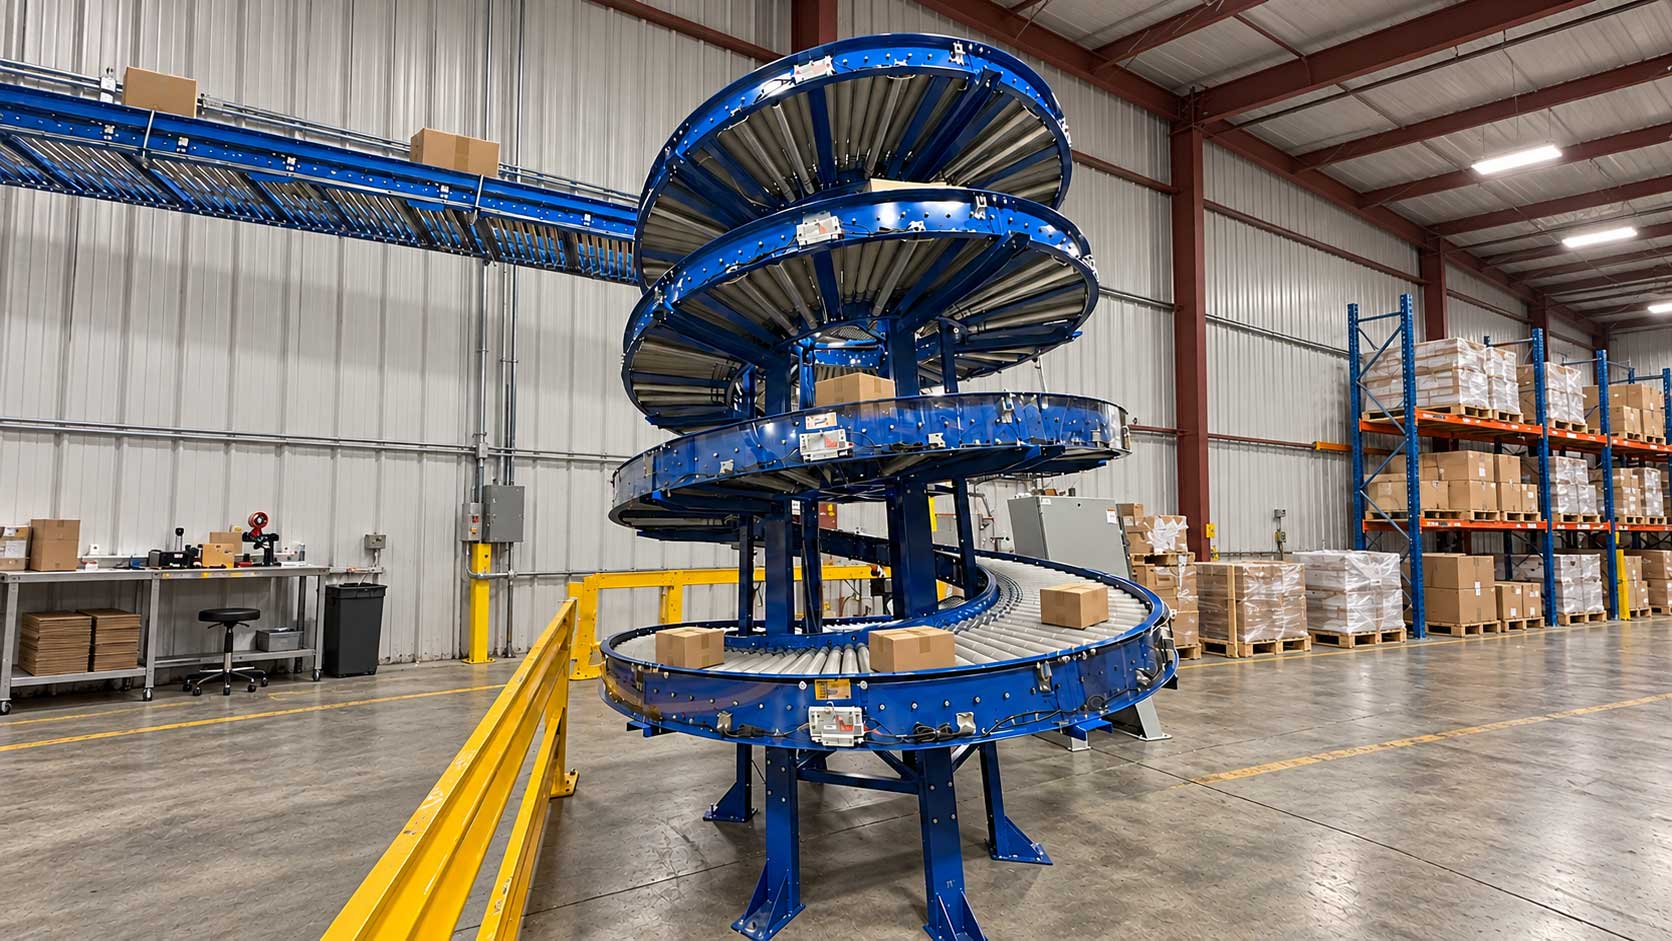
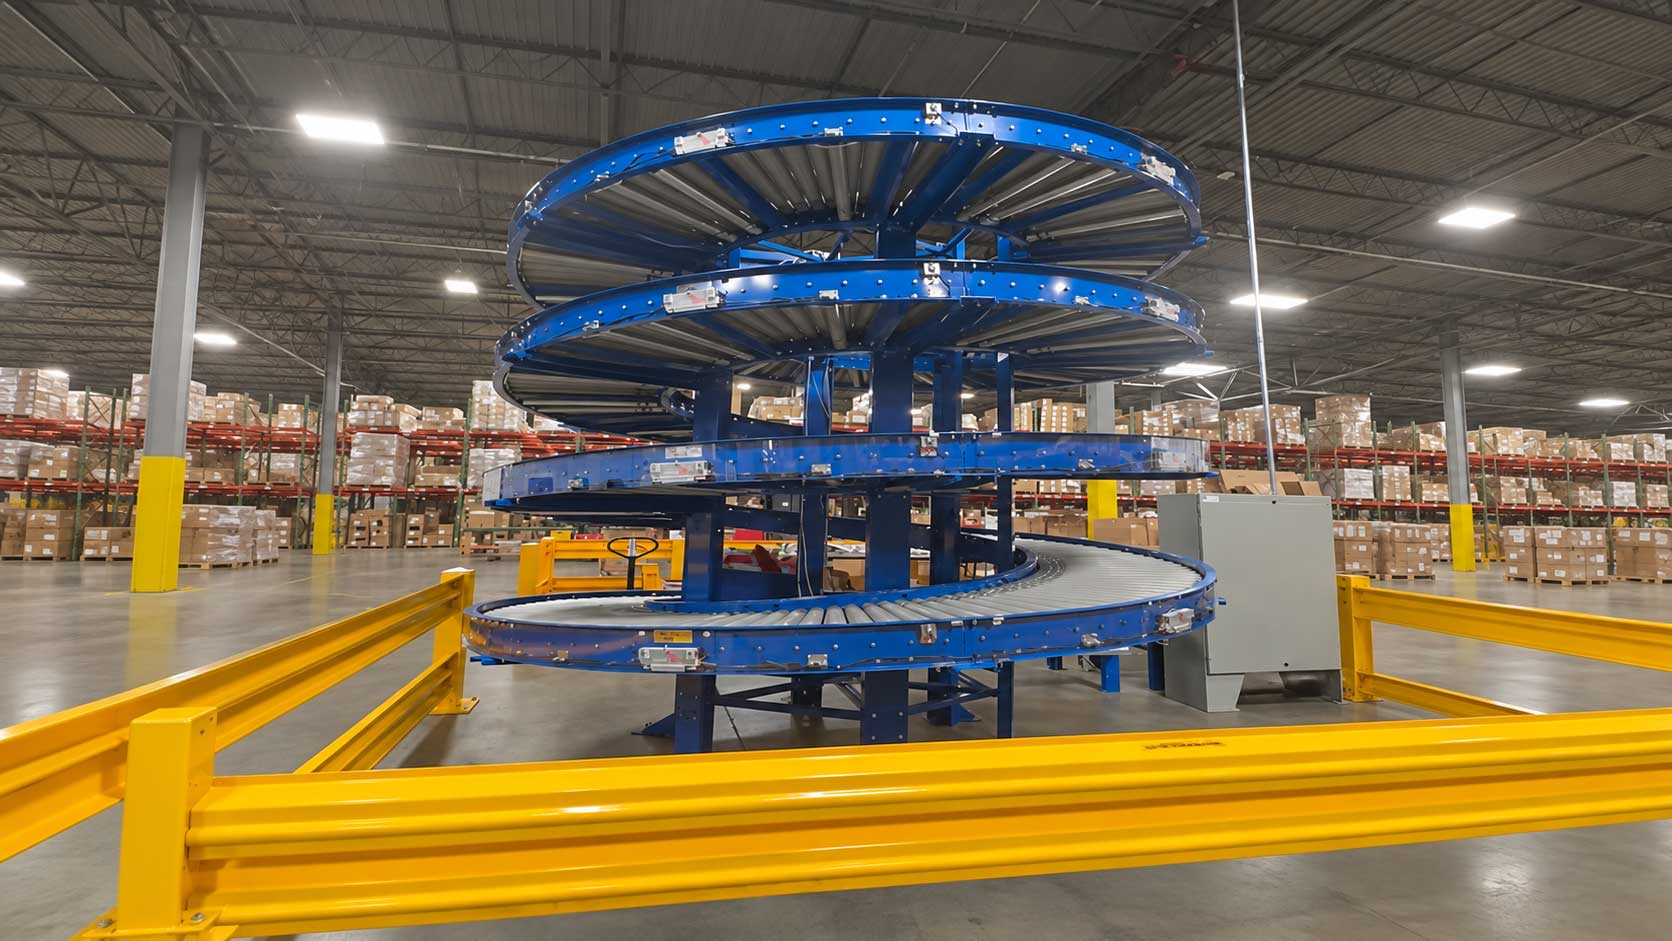
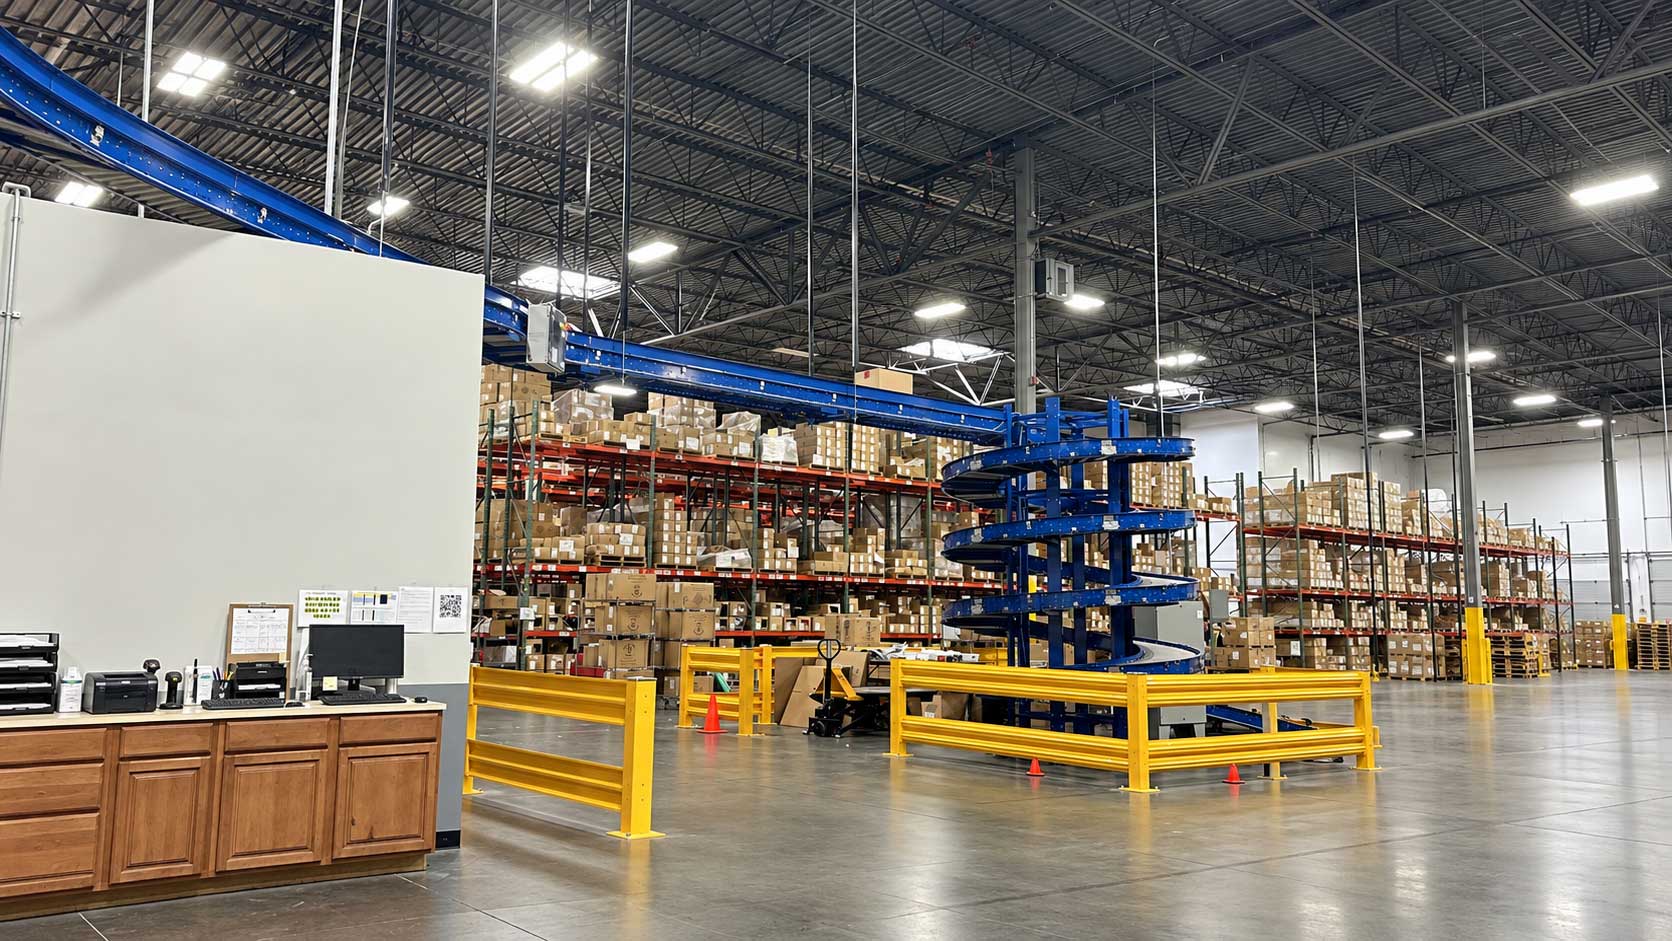
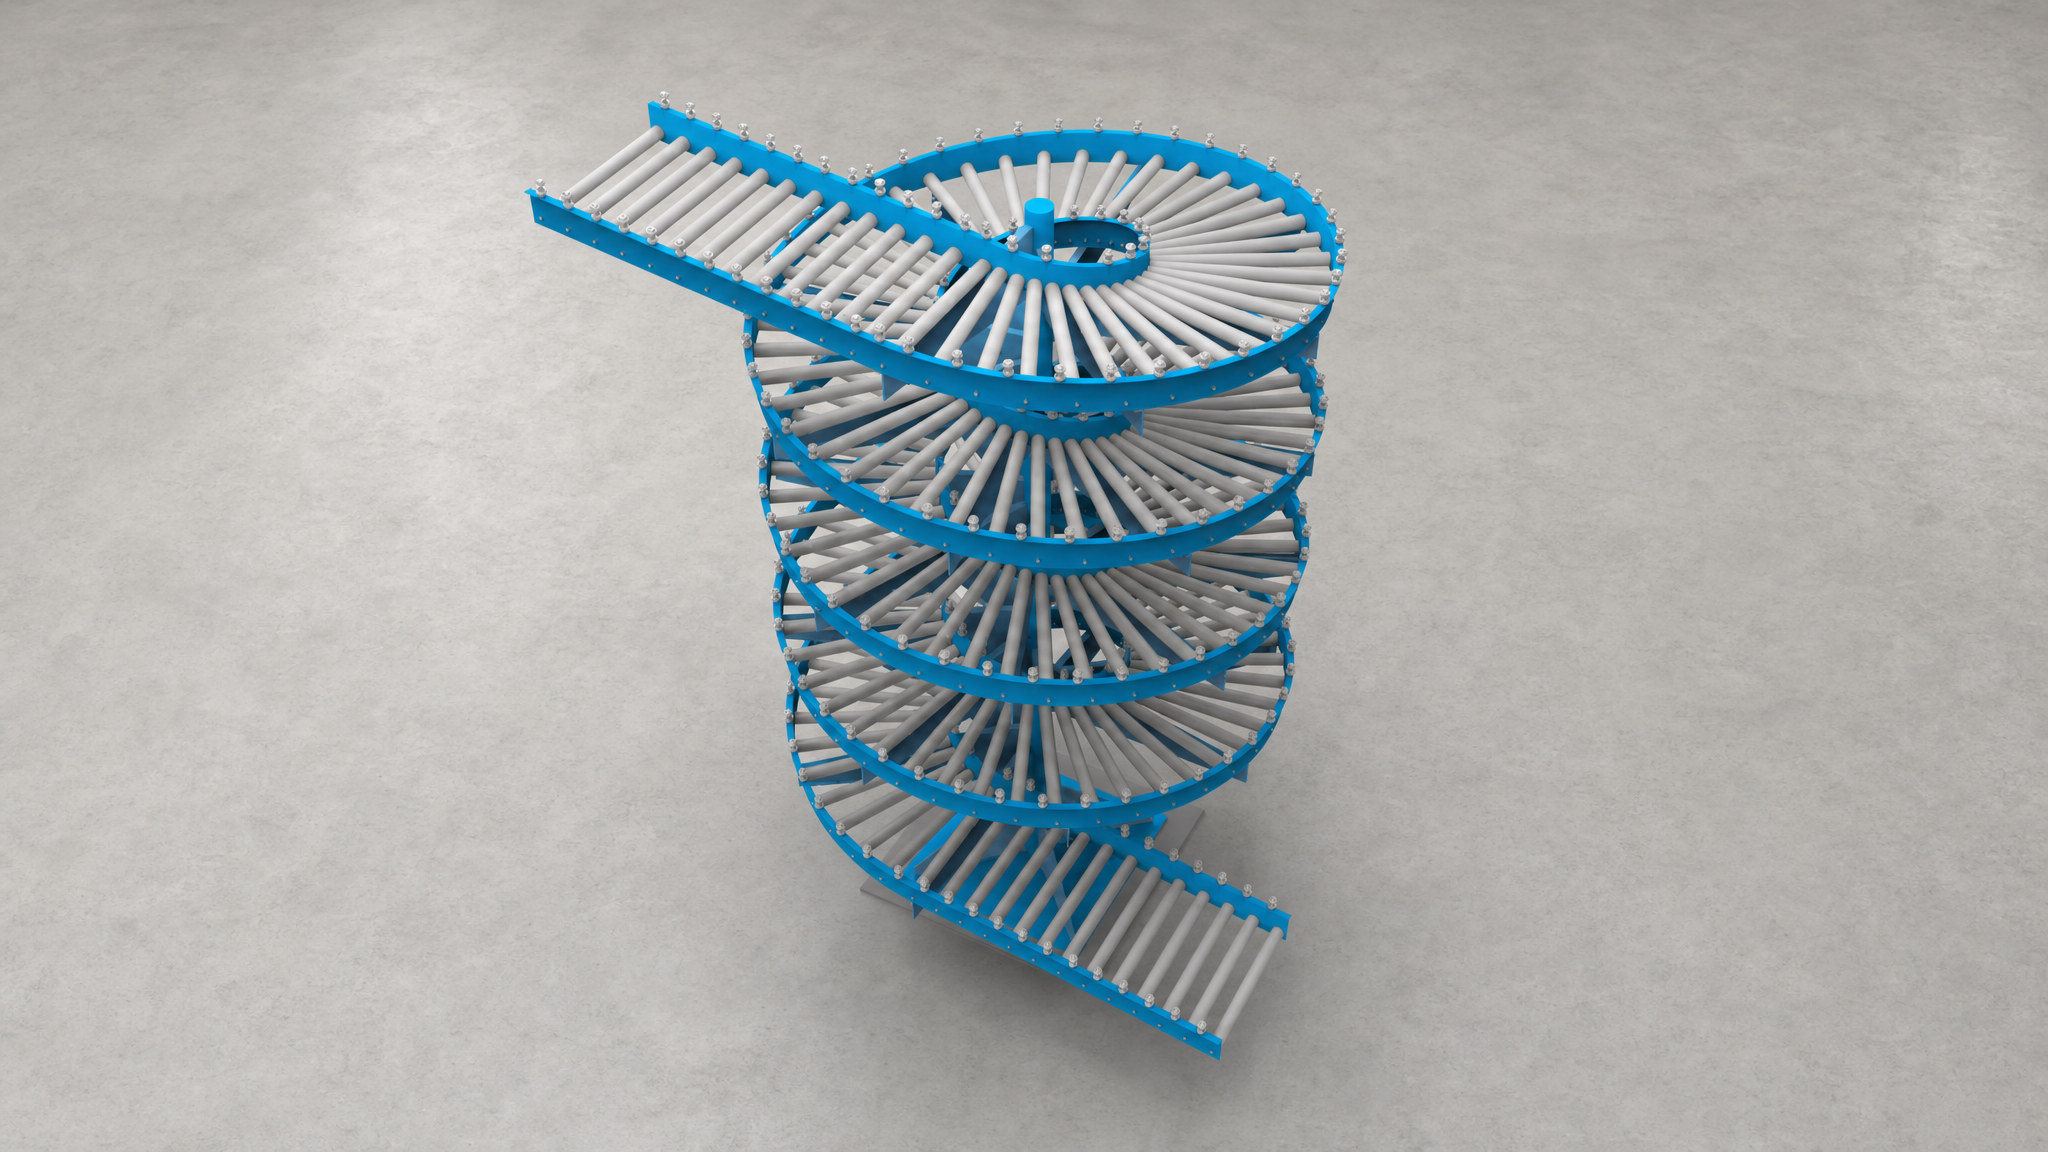
A spiral conveyor is a continuous vertical conveyor system that moves lighter cartons, cases, or totes upward or downward along a circular spiral path. It is used when a facility needs to connect different elevations without the floor space required for a long incline conveyor.
Spiral Conveyor Design Inputs: Containers, Elevation, and Footprint
Spiral conveyor design starts with the load and the route. Project planning should confirm the container profile, vertical travel path, available footprint, and how the conveyor will connect to upstream and downstream equipment.
- Carton, case, or tote dimensions, weight range, and bottom condition
- Entry and exit elevations, transfer direction, and required handoff points
- Available floor space, overhead clearances, and surrounding equipment
- Connection requirements for new conveyor layouts or existing conveyor systems
Spiral Conveyor Options and System Interfaces
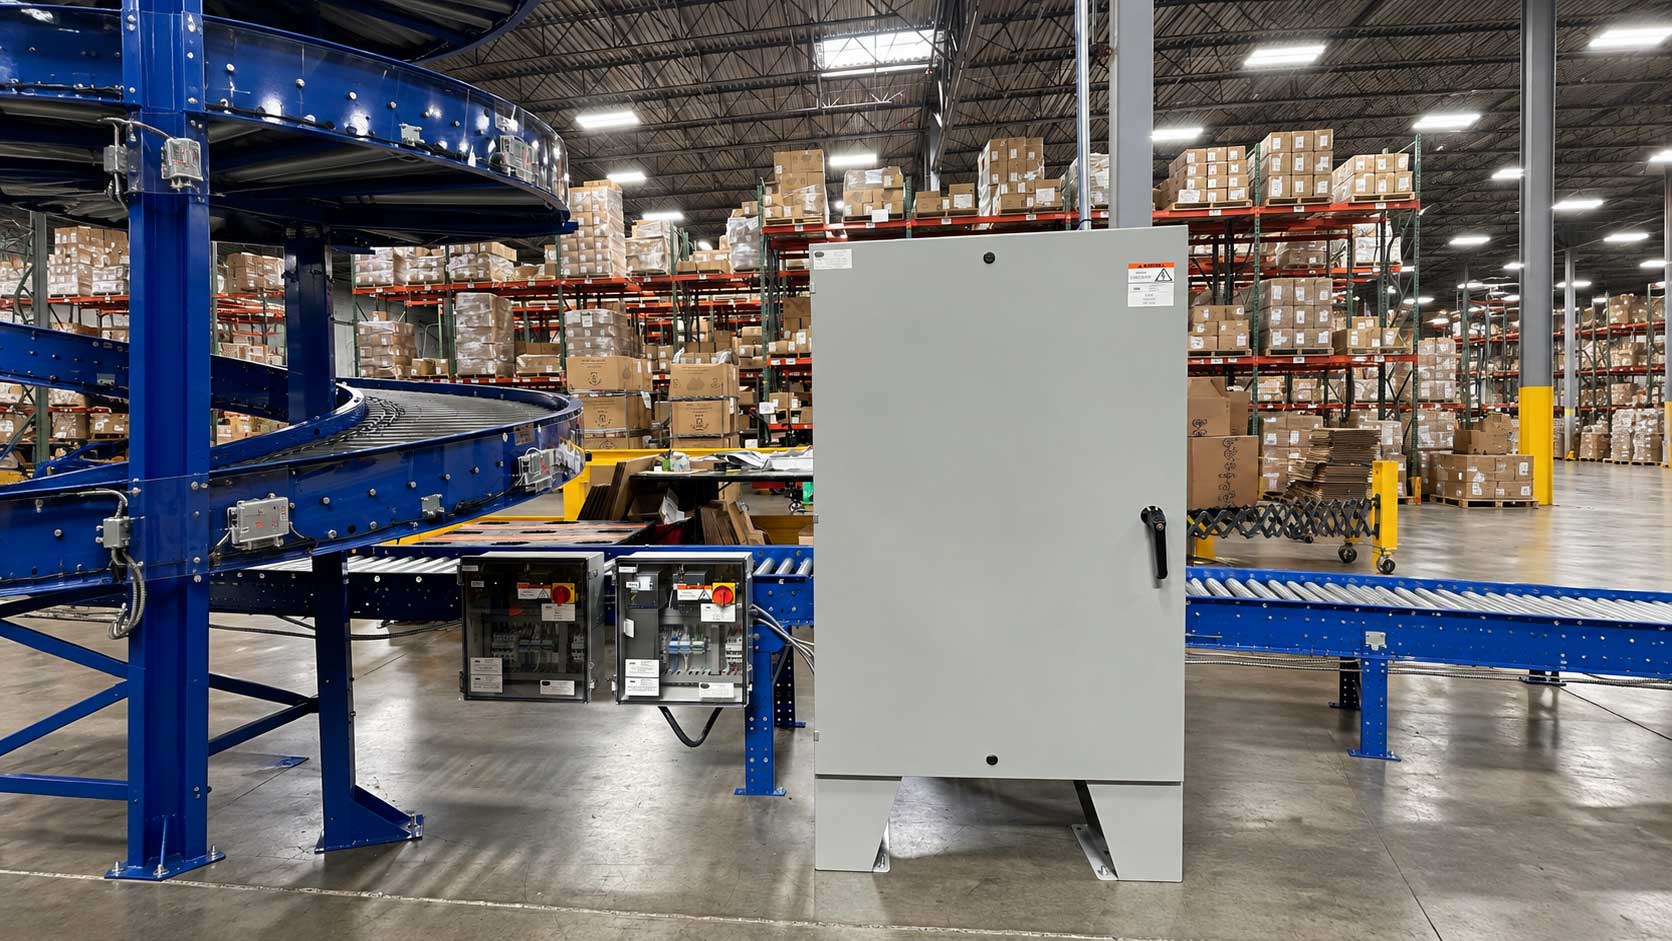
A spiral conveyor system can be configured around the movement method and transfer layout needed for the application. The selection depends on the container, route, elevation change, and whether the project is part of a new conveyor layout or a retrofit.
- Motor-driven rollers (MDR) for moving lighter cartons and cases through the spiral path
- Gravity-assisted movement for applications where the load, route, and transfer conditions allow it
- Custom entry and exit transfer points to match the facility layout
- Integration with new conveyor systems or older conveyor equipment
Where Spiral Conveyors Fit in Facility Workflows
Spiral conveyors fit warehouses, distribution centers, manufacturing plants, and commercial facilities that need vertical case or tote movement in a compact footprint. They are especially useful in multi-level layouts where materials must move between work areas without dedicating long runs of floor space to an incline.
- Moving cases or totes between a warehouse floor and a mezzanine
- Connecting picking, packing, or shipping areas located at different elevations
- Transferring containers between production and packaging areas
- Adding vertical movement where existing equipment limits available floor space
Planning a Spiral Conveyor System
Before requesting a spiral conveyor quote, gather facility drawings, container details, entry and exit elevations, and information about the conveyor lines that will feed or receive product. Our specialists can review clearances, transfer points, and layout constraints to recommend a practical spiral conveying solution.
- Whether the project is new construction, an expansion, or a retrofit
- The direction of product movement and the elevations to be connected
- Space restrictions around columns, walls, work areas, or existing equipment
- Interface requirements for current or planned conveyor systems
Warehouse Case Movement Between Levels

Warehouse teams use spiral conveyors when cartons, cases, or totes must travel between a floor-level conveyor and an elevated work area. The compact spiral path preserves usable floor space that would otherwise be taken by a long incline.
- Useful for multi-level storage, picking, or packing areas
- Supports upward or downward case and tote movement
- Requires review of mezzanine height, transfer points, and clearances


Planning Your Spiral Conveyor System
Use these planning decisions to define a spiral conveyor configuration for your facility. Final recommendations depend on the load, elevation change, footprint, clearances, and conveyor interfaces.
| Planning Decision | Why It Matters | What to Confirm |
|---|---|---|
| Container Profile | Confirming whether cartons, cases, or totes can move reliably through the spiral path. | Review dimensions, weight range, bottom condition, and handling requirements before selecting the conveyor approach. |
| Elevation and Transfers | Defining how product enters and exits the spiral conveyor. | Confirm entry height, exit height, flow direction, and transfer point locations early in layout planning. |
| Footprint and Clearance | Facilities where a long incline conveyor would take too much floor space. | Measure available floor area, overhead clearances, and nearby equipment to verify fit. |
| Movement Method | Choosing between powered MDR roller movement and gravity-assisted movement where appropriate. | The right method depends on the container, route, elevation change, and transfer conditions. |
| Existing System Interfaces | Retrofits or expansions that connect the spiral conveyor to older or new conveyor lines. | Review upstream and downstream equipment so transfer points match the current or planned material flow. |
Southwest Solutions Near You
With 7 offices in Texas, Oklahoma, Kansas and Colorado, plus teams covering every major metro area nationwide, Southwest Solutions Group delivers expert spiral conveyor sales, design, installation, and maintenance support wherever you need it.
Spiral Conveyor Service Areas
Texas
- Dallas
- Austin
- Houston
- San Antonio
- Waco
- Tyler
- Amarillo
- Lubbock
- El Paso
- Ft Worth
- Corpus Christi
- Midland
Oklahoma
- Oklahoma City
- Tulsa
- Norman
- Lawton
- Enid
- Stillwater
- McAlester
- Muskogee
- Guymon
Kansas
- Wichita
- Overland Park
- Topeka
- Kansas City
- Lawrence
- Manhattan
- Salina
- Hays
- Dodge City
- Garden City
Colorado
- Denver
- Colorado Springs
- Fort Collins
- Grand Junction
- Pueblo
- Durango
- Alamosa
- Steamboat Springs
- Greeley
Alabama
- Huntsville
- Birmingham
- Montgomery
- Mobile
- Tuscaloosa
- Hoover
- Dothan
- Decatur
Alaska
- Anchorage
- Fairbanks
- Juneau
- Sitka
- Ketchikan
- Kodiak
- Bethel
- Nome
Arizona
- Phoenix
- Tucson
- Flagstaff
- Yuma
- Prescott
- Lake Havasu City
- Sierra Vista
- Kingman
Arkansas
- Little Rock
- Fayetteville
- Fort Smith
- Jonesboro
- Hot Springs
- Pine Bluff
- Texarkana
- Bentonville
- Arkadelphia
California
- Los Angeles
- San Diego
- San Francisco
- Sacramento
- Fresno
- Redding
- Bakersfield
- San Bernardino
- San Jose
Connecticut
- Hartford
- New Haven
- Stamford
- Bridgeport
Delaware
- Wilmington
- Dover
- Newark
- Rehoboth Beach
Florida
- Jacksonville
- Tallahassee
- Orlando
- Tampa
- Miami
- West Palm Beach
- Fort Myers
- Pensacola
Georgia
- Atlanta
- Savannah
- Augusta
- Columbus
- Macon
- Athens
- Valdosta
- Gainesville
- Albany
Hawaii
- Honolulu
- Hilo
- Kahului
- Kailua-Kona
- Lihue
Idaho
- Boise
- Coeur d'Alene
- Twin Falls
- Idaho Falls
- Pocatello
- Lewiston
- McCall
- Sandpoint
- Moscow
Illinois
- Chicago
- Springfield
- Rockford
- Peoria
- Champaign
- Bloomington
- Carbondale
- Moline
- Quincy
Indiana
- Indianapolis
- Fort Wayne
- South Bend
- Evansville
- Lafayette
- Bloomington
- Terre Haute
- Gary
- Muncie
Iowa
- Des Moines
- Cedar Rapids
- Davenport
- Sioux City
- Iowa City
- Waterloo
- Council Bluffs
- Ames
- Mason City
Kentucky
- Louisville
- Lexington
- Bowling Green
- Owensboro
- Covington
- Paducah
- Ashland
- Richmond
- Frankfort
- Pikeville
- Florence
Louisiana
- New Orleans
- Baton Rouge
- Shreveport
- Lafayette
- Lake Charles
- Monroe
- Alexandria
- Houma
Maine
- Portland
- Bangor
- Augusta
- Lewiston
- Waterville
- Presque Isle
- Bar Harbor
- Biddeford
- Rockland
Maryland
- Baltimore
- Annapolis
- Frederick
- Hagerstown
- Salisbury
Massachusetts
- Boston
- Worcester
- Springfield
- Pittsfield
Michigan
- Detroit
- Grand Rapids
- Lansing
- Ann Arbor
- Flint
- Traverse City
- Marquette
- Kalamazoo
- Saginaw
Minnesota
- Minneapolis
- St. Paul
- Duluth
- Rochester
- Mankato
- St. Cloud
- Bemidji
- Moorhead
Mississippi
- Jackson
- Gulfport
- Hattiesburg
- Biloxi
- Southaven
- Meridian
- Tupelo
- Natchez
- Greenville
- Oxford
Missouri
- Jefferson City
- St. Louis
- Kansas City
- Springfield
- Columbia
- Joplin
- Cape Girardeau
- St. Joseph
- Rolla
Montana
- Helena
- Billings
- Missoula
- Great Falls
- Bozeman
- Kalispell
- Havre
- Miles City
Nebraska
- Lincoln
- Omaha
- Grand Island
- Kearney
- Scottsbluff
- Norfolk
- North Platte
- Fremont
- South Sioux City
Nevada
- Las Vegas
- Reno
- Carson City
- Elko
- Pahrump
- Henderson
- Winnemucca
- Mesquite
- Fallon
New Hampshire
- Concord
- Manchester
- Portsmouth
- Keene
- Nashua
New Jersey
- Newark
- Jersey City
- Trenton
- Atlantic City
New Mexico
- Santa Fe
- Albuquerque
- Las Cruces
- Roswell
- Farmington
- Gallup
- Carlsbad
- Clovis
New York
- Albany
- New York City
- Buffalo
- Rochester
- Syracuse
- Binghamton
- Ithaca
- Plattsburgh
North Carolina
- Raleigh
- Charlotte
- Greensboro
- Asheville
- Wilmington
- Fayetteville
- Boone
- Greenville
North Dakota
- Bismarck
- Fargo
- Grand Forks
- Minot
- Dickinson
- Williston
- Jamestown
- Devils Lake
Ohio
- Columbus
- Cleveland
- Cincinnati
- Toledo
- Dayton
- Akron
- Youngstown
- Athens
Oregon
- Portland
- Salem
- Eugene
- Hermiston
- Baker City
- Medford
- Bend
- Klamath Falls
Pennsylvania
- Harrisburg
- Philadelphia
- Pittsburgh
- Erie
- Scranton
- State College
- Allentown
- Williamsport
Rhode Island
- Providence
- Warwick
- Newport
- Woonsocket
South Carolina
- Columbia
- Charleston
- Greenville
- Myrtle Beach
- Hilton Head Island
- Spartanburg
- Florence
- Rock Hill
South Dakota
- Pierre
- Sioux Falls
- Rapid City
- Aberdeen
- Watertown
- Brookings
- Mitchell
- Yankton
Tennessee
- Memphis
- Jackson
- Nashville
- Clarksville
- Cookeville
- Chattanooga
- Knoxville
- Johnson City
Utah
- Salt Lake City
- Ogden
- Logan
- Provo
- St. George
- Cedar City
- Moab
- Vernal
Vermont
- Montpelier
- Burlington
- Rutland
- Brattleboro
Virginia
- Richmond
- Norfolk
- Virginia Beach
- Roanoke
- Lynchburg
- Harrisonburg
- Fredericksburg
- Bristol
Washington
- Olympia
- Seattle
- Spokane
- Yakima
- Bellingham
- Wenatchee
- Kennewick
- Vancouver
West Virginia
- Charleston
- Huntington
- Morgantown
- Wheeling
- Parkersburg
- Beckley
- Martinsburg
- Bluefield
Wisconsin
- Madison
- Milwaukee
- Green Bay
- Eau Claire
- La Crosse
- Wausau
- Appleton
- Superior
Wyoming
- Cheyenne
- Casper
- Laramie
- Gillette
- Sheridan
- Rock Springs
- Jackson
- Cody
District of Columbia
- Washington D.C.
Frequently Asked Questions
A spiral conveyor is used to move cartons, cases, or totes vertically between different elevations in a facility. It is commonly used in multi-level warehouses, distribution centers, manufacturing plants, and commercial facilities where floor space is limited.
A vertical spiral conveyor moves products along a circular spiral path, allowing cartons, cases, or totes to travel upward or downward between facility levels. This layout provides a compact alternative to a long incline conveyor.
Useful design information includes container type and dimensions, weight range, entry and exit elevations, available floor space, clearances, and details about upstream and downstream conveyor interfaces.
Yes, spiral conveyor systems can be integrated with new or existing conveyor layouts. During planning, transfer points, footprint, clearances, and equipment interfaces are reviewed to confirm fit.
A spiral conveyor is often preferred when vertical movement is needed but floor space is limited. Its circular path can connect elevations in a smaller footprint than a long incline conveyor.
No. Spiral conveyors provide continuous movement for cartons, cases, or totes along a spiral path. Platform lifts and VRCs move loads intermittently on a platform, so they serve different material handling needs.
Explore More Specialty Products
Case and Tote Conveyors
Case and tote conveyors move cartons and reusable totes between work areas, reducing manual handling while supporting controlled staging, transfers, and routing throughout a facility.
Explore Case and Tote Conveyors
Catwalk Racking Systems
Catwalk racking systems maximize vertical storage with multi-level shelving, stairs, and aisles, providing organized manual access where floor space is limited in warehouses.
Explore Catwalk Racking Systems
Data Center Cages
Modular wire mesh panels create secure, visible enclosures for servers and equipment, supporting controlled access, airflow, and flexible layouts in data centers.
Explore Data Center Cages
Directional Fans
Directional fans provide precise, high-velocity airflow to targeted zones like aisles or workstations, overcoming obstructions where broad-area fans fall short.
Explore Directional Fans
Dumbwaiter
Compact goods-only lift for vertical transfer of supplies, food, documents, and small materials between floors in commercial and residential buildings.
Explore Dumbwaiters
Flat File Dolly
A flat file dolly provides a durable rolling base to safely move compatible flat-file cabinets, enhancing mobility for large artwork, maps, and documents.
Explore Flat File Dolly
Floor Cable Raceways
Floor cable raceways deliver organized power and data routing across floors, ideal for flexible layouts in offices, conference rooms, and public spaces.
Explore Floor Cable Raceways
Freight Elevator
Freight elevators provide a dedicated vertical route for moving equipment, supplies, and materials between floors, streamlining goods transport in commercial and industrial facilities.
Explore Freight Elevators
HVLS Fans
HVLS fans provide efficient ceiling-mounted air circulation for warehouses, industrial plants, and commercial spaces without occupying valuable floor space or creating aisle obstructions.
Explore HVLS Fans
Mezzanine Platforms
Mezzanine platforms create elevated deck space for storage, work, or staging, helping facilities expand usable area without increasing the building footprint or disrupting operations.
Explore Mezzanine Platforms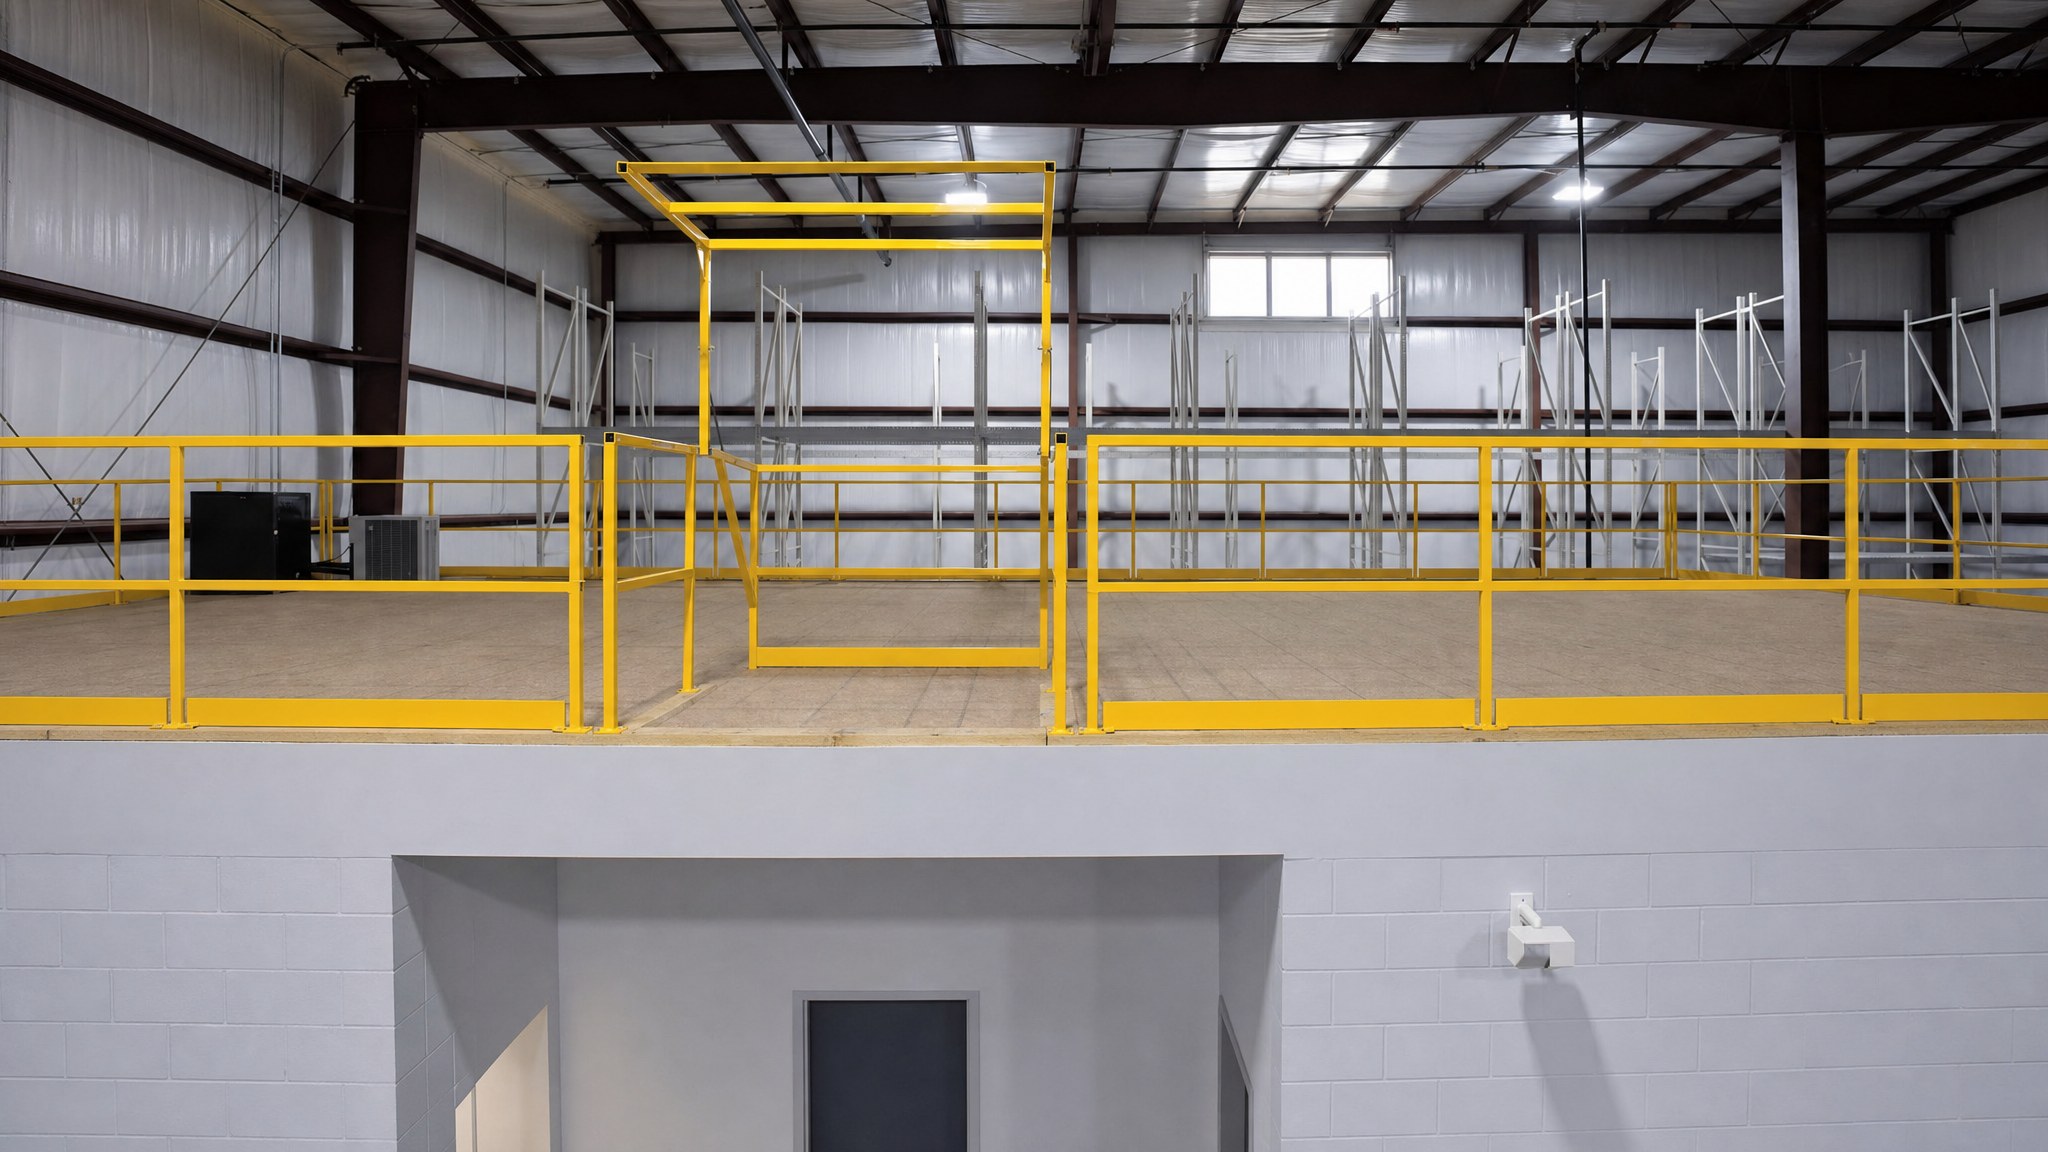
Mezzanine Safety Gates
Mezzanine safety gates control elevated loading openings during material transfers, with gate styles selected around load size, forklift access, and operating workflow.
Explore Mezzanine Safety Gates
Rack Supported Mezzanines
Rack-supported mezzanines add elevated storage or work space above existing racks, maximizing vertical capacity while preserving access to lower-level inventory and aisles.
Explore Rack Supported Mezzanines
Vertical Reciprocating Conveyor
Safely move materials between floors with a vertical reciprocating conveyor. Handles loads from boxes to pallets up to 30,000 lbs, customizable for facility layouts.
Explore Vertical Reciprocating Conveyor
Automated Labeling Systems
Print barcode and RFID labels for files, products, or shipments. Fast, accurate systems that cut manual steps and reduce labeling errors.
Explore Automated Labeling Systems
Document Scanning Services
Convert paper records into secure, searchable digital files with professional scanning, indexing, quality checks, and encrypted delivery.
Explore Document Scanning Services
Wire Partition Cages & Lockers
Welded wire enclosures for tools, evidence, or server areas. Modular, secure, and compliant with DEA, IT, and facility safety standards.
Explore Wire Partition Cages & Lockers
Hanging Gun Bags
Tamper-resistant hanging gun bags provide efficient firearm storage for pistols and rifles. Perfect for evidence handling in police and public safety departments.
Explore Hanging Gun Bags
Hospital Bed Lift
Save floor space and reduce hallway clutter by stacking unused hospital beds in a secure vertical lift system for efficient storage and maintenance access.
Explore Hospital Bed Lift
Industrial Stairs
OSHA-compliant industrial stairs and work platforms engineered for safe, modular access to elevated spaces in warehouses, factories, and service facilities.
Explore Industrial Stairs
Inmate Property Bags
Durable inmate property bags with secure zip closures, ID sleeves, and reinforced handles for organized storage on shelves, in bins, or in transport.
Explore Inmate Property Bags
Lab Sterilizers
Safely sanitize mobile devices, lab tools, and office equipment with eco-friendly UVC technology in a sleek, compact cabinet design.
Explore Lab Sterilizers
Mezzanine, Material Lifts & Conveyors
Create second-level platforms, move pallets between floors, or automate product flow. Modular and code-compliant systems that scale with you.
Explore Mezzanine, Material Lifts & Conveyors
Raised Access Floor System
Modular raised floors conceal wiring, HVAC, and power underfoot while allowing quick access and easy reconfiguration as your needs change.
Explore Raised Access Floor System
RFID & Barcode Tracking Software
Track inventory, files, or tools with RFID portals and barcode scans. Real-time visibility helps reduce loss and improve efficiency.
Explore RFID & Barcode Tracking Software
Roll-Down Security Doors
Lockable roll-down shutters for service counters, cabinets, and secure rooms. Available in manual or motorized models with safety features.
Explore Roll-Down Security Doors
Shoe Cover Dispenser
Maintain clean, safe environments with hands-free shoe cover dispensers and durable covers for labs, clinics, cleanrooms, and visitor spaces.
Explore Shoe Cover Dispenser
Solar Canopy
Modular solar canopy systems offering protection and renewable energy for parking, loading docks, and outdoor walkways in commercial facilities.
Explore Solar CanopyPlan a Spiral Conveyor for Your Facility
Ready to move cases or totes between facility elevations with a spiral conveyor? Our experts can help you evaluate your layout and requirements.
Share your container details, entry and exit elevations, transfer points, and available footprint to get started.
Call us at (800) 803-1083 or Contact Us to schedule your free consultation today.
Request a Spiral Conveyor Consultation